
Porosity is one of the most frustrating defects in lost wax jewelry casting. A casting may look acceptable when it comes out of the flask, only for small pits, holes, or deeper cavities to appear during filing and polishing.
The challenge is that porosity is not one single defect. Similar-looking problems can result from different combinations of sprue design, solidification, metal condition, temperature, investment preparation, burnout, mold conditions, and the casting process itself.
Quick Answer: What Causes Porosity in Jewelry Casting?
Common areas to investigate include:
- Sprue size, placement, and feeding
- Solidification around heavier sections of the casting
- Metal cleanliness and alloy condition
- Metal and flask temperature
- Investment preparation
- Incomplete or unsuitable burnout
- Gas-generating reactions involving the metal, residues, and investment
- Mold permeability and evacuation
- Pattern surface defects or contamination
- Vacuum-system leaks or poor sealing in vacuum-assisted casting
There is no single adjustment that fixes every case. Increasing temperature, increasing vacuum, or changing the burnout schedule without first identifying the likely defect mechanism can make troubleshooting more difficult.
Gas-Related vs. Shrinkage-Related Porosity
A useful starting point is to determine whether the defect appears more consistent with gas-related porosity or shrinkage-related porosity. This distinction helps guide troubleshooting, but it should not be treated as an absolute visual test.
Gas-Related Porosity
Gas-related pores are often relatively round or smooth, although their appearance can vary.
Gas-related porosity can result from several mechanisms, including gases associated with the molten metal, gas entrainment during metal flow, residual pattern material, contamination, and reactions between the molten alloy and investment material.
Possible areas to investigate include:
- Metal cleanliness and contamination
- Condition of recycled metal
- Melting and pouring practices
- Excessive or unsuitable process temperatures
- Incomplete burnout
- Residual wax, resin, or carbonized material
- Investment condition and permeability
- Turbulent metal flow
With some gypsum-bonded investment systems, thermal decomposition and reactions involving residual pattern material can also contribute to gas-related casting defects under certain conditions.
Shrinkage-Related Porosity
Metals contract as they solidify. During this stage, sections that are still solidifying need an adequate supply of liquid metal.
If the feeding path freezes too early, the remaining contraction may not be compensated, leaving shrinkage cavities inside or near the surface of the casting.
Shrinkage-related porosity is often more irregular in appearance and may be concentrated around heavier sections of a piece. However, appearance alone is not enough for a definitive diagnosis.
If defects repeatedly occur in a thick section, near an abrupt change in cross-section, or in the same location on repeated castings, the sprue and local solidification behavior should be high on the troubleshooting list.
Where Should You Start Troubleshooting?
Porosity can occur alongside other casting defects. Incomplete filling and rough surfaces, for example, are not themselves types of porosity, but they can provide useful clues because some of the same process variables may be involved.
| What You See | Possible Direction to Investigate | What to Check |
|---|---|---|
| Round, relatively smooth pores | Gas-related porosity may be involved | Metal condition, melting, burnout, investment, process temperature |
| Irregular cavities, especially in heavier sections | Investigate shrinkage and feeding | Sprue size, position, feeding path, and solidification |
| Defects concentrated near thick sections | Localized feeding or solidification problem may be involved | Sprue placement, section thickness, and thermal conditions |
| Fine pits or rough surface | Possible surface porosity or another surface defect; several causes are possible | Burnout, investment, contamination, and metal/mold interaction |
| Thin details do not fill completely | Related incomplete-filling defect | Metal and flask temperature, sprueing, mold evacuation, and casting conditions |
| Holes appear after filing or polishing | Subsurface porosity may have been exposed | Pore shape, location, distribution, and process records |
| The same defect repeatedly appears in the same location | Geometry or process-related cause may be involved | Pattern surface, sprue position, local section thickness, and solidification |
These observations are troubleshooting clues rather than guarantees. More than one cause can contribute to the same casting.
1. Check the Sprue and Feeding System
Sprue design is one of the first areas to investigate when shrinkage-related porosity is suspected.
A feed sprue does more than carry molten metal into the mold. It also needs to provide liquid metal while the casting is solidifying and contracting.
If the feed path freezes before a heavier section has finished solidifying, that section may no longer receive enough liquid metal to compensate for contraction.
Common Areas to Check
- Sprues that may be too thin for the section being fed
- Excessively long or restrictive feed paths
- Sprue placement relative to heavier sections
- Abrupt changes in section thickness
- Sharp or poorly designed transitions
- Complex pieces that may require a different feeding arrangement
There is no universal sprue diameter or layout that is correct for every jewelry design. Pattern geometry, alloy, casting method, and thermal conditions all affect feeding requirements.
2. Check the Metal and Melting Process
Metal condition is another important variable. Recycled material can carry investment residue, oxides, contamination, or other material from previous processing if it has not been properly prepared.
Different alloys and suppliers may also have different recommendations for the use of recycled material, so there is no reliable universal rule for how many times jewelry metal can be remelted.
When troubleshooting, record:
- The alloy being cast
- New versus recycled metal used in the charge
- Condition and cleanliness of recycled material
- Previous processing history when known
- Crucible condition
- Melting method
- Flux practice, if applicable to the alloy and process
Follow the alloy supplier's recommendations for remelting and metal preparation whenever available.
3. Review Metal Temperature
When a casting fails to fill properly, increasing metal temperature can seem like the obvious solution. In some cases, insufficient temperature may contribute to premature solidification and incomplete filling.
However, excessive temperature can also increase unwanted metal/mold interaction and alter solidification behavior. Higher temperature is therefore not a universal solution for porosity.
The appropriate processing range depends on factors such as:
- Alloy composition
- Pattern geometry
- Section thickness
- Flask temperature
- Investment system
- Casting method
- Equipment configuration
Start with the processing range recommended by the alloy and investment manufacturers and make controlled adjustments when troubleshooting.
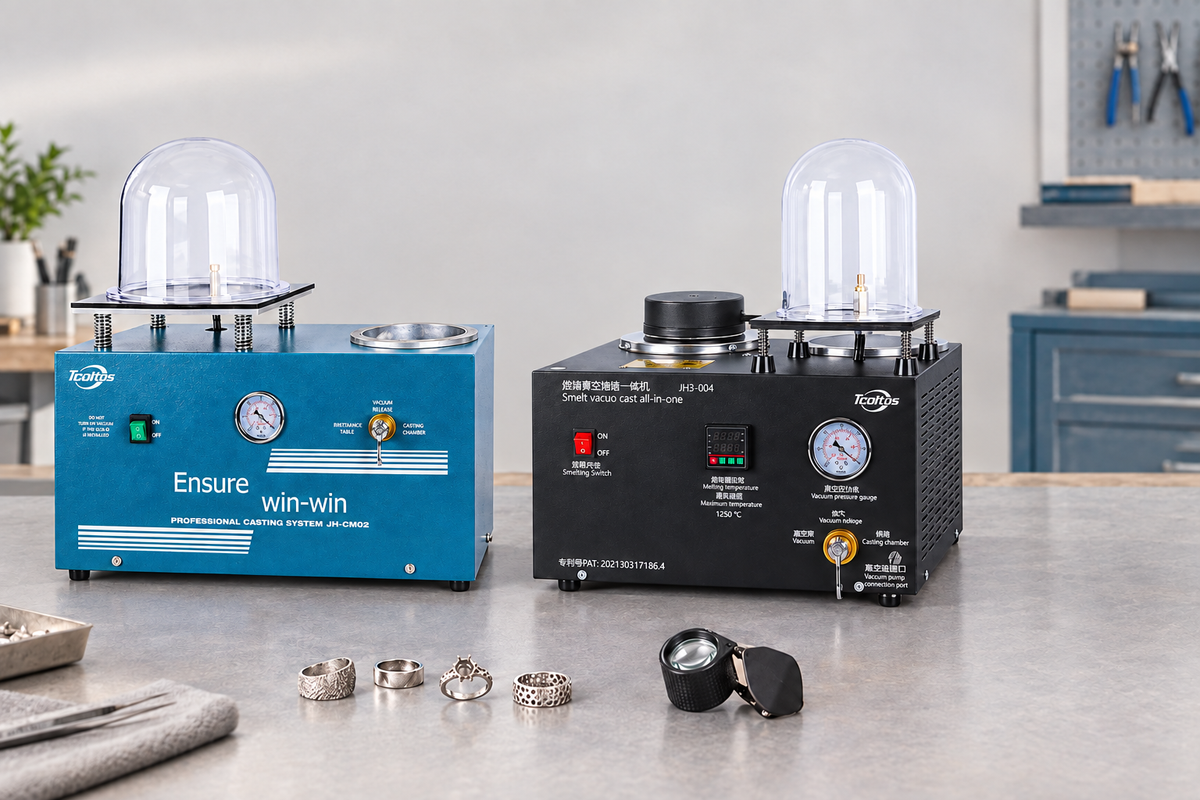
Related melting and vacuum casting equipment

1050°C Jewelry Vacuum Casting and Melting Machine | 1–3KG Crucible
Review the product specifications and operating instructions for your alloy and casting setup. A temperature setting alone does not determine the correct casting conditions or eliminate porosity.
4. Review Flask Temperature
Flask temperature and metal temperature work together and should not be considered independently.
A hotter mold generally delays solidification and may help molten metal reach fine sections. A cooler mold promotes faster heat extraction. Neither condition is automatically better.
The appropriate flask temperature depends on the alloy, pattern geometry, section thickness, investment system, casting method, and manufacturer recommendations.
Avoid copying another caster's flask temperature without knowing the rest of their process.
5. Review the Burnout Cycle
Reaching the furnace's final set temperature does not, by itself, confirm that burnout has been completed successfully.
Burnout requires an appropriate combination of temperature, time, pattern material, flask size, furnace conditions, and investment requirements.
Check the Following
- The investment manufacturer's burnout schedule
- Pattern material: wax or castable resin
- Heating rate
- Intermediate hold stages
- Hold times
- Maximum permitted temperature
- Flask size
- Number of flasks and overall furnace loading
- Furnace airflow or ventilation requirements specified by the manufacturer
- Final flask temperature before casting
Residual wax, resin, or carbonized material can contribute to casting problems. With some gypsum-bonded investment systems, reactions involving the investment and residual pattern material may also contribute to gas-related porosity and poor surface quality.
Burnout requirements can differ substantially between conventional wax and castable resins. Follow the instructions for the specific investment and pattern material being used rather than assuming that one burnout schedule is suitable for every application.
6. Check Investment Preparation and Mold Permeability
Investment preparation affects mold strength, surface quality, dimensional behavior, and the movement of gases through the mold during casting.
Review:
- Powder-to-water ratio
- Water temperature
- Mixing time
- Working time
- Vacuum-investing procedure
- Setting time
- Storage condition of the investment powder
- Burnout procedure
Do not intentionally change the powder-to-water ratio outside the manufacturer's specification simply to make the mold more permeable. Changing the ratio can also affect mold strength, expansion, and surface quality.
Related casting flask

Tooltos 3.5in Perforated Casting Flask | Flanged Vacuum 4-10 Inch
Check the selected flask height, flange fit, and your machine's maximum flask dimensions before ordering. Flask selection does not replace correct investment preparation or feeding design.
7. Check the Vacuum System
In vacuum-assisted casting, the vacuum system helps evacuate air through the porous investment and assists molten metal in filling the mold.
A leaking or poorly performing system can contribute to mold-filling problems, particularly with fine or complex patterns. However, low vacuum should not automatically be diagnosed as the cause of porosity.
Check the Complete Vacuum Path
- Vacuum pump condition
- Hoses and fittings
- Gaskets and seals
- Flask seating
- Casting-table or chamber seal
- Vacuum gauge behavior
- Vacuum stability with the casting setup assembled
A dry test can help identify obvious leaks in the vacuum system, but it does not fully reproduce actual hot-flask casting conditions. Follow the equipment manufacturer's inspection and test procedures whenever available.
Related vacuum casting equipment

Tooltos 2L Jewelry Vacuum Investing and Casting Machine with Built-In Pump | 3 CFM
Review the machine specifications and operating instructions for your casting setup. Vacuum equipment supports investing and mold filling; it is not a universal cure for casting porosity.
8. Inspect the Wax or Resin Pattern
Some defects visible in the final casting originate in the pattern rather than during metal solidification.
Inspect the pattern carefully for:
- Surface pits or bubbles
- Cracks
- Missing or poorly formed details
- Support-removal damage on printed patterns
- Surface contamination or residue
- Unintended geometry or deformation
Surface defects in a wax or resin pattern can be reproduced in the investment mold and appear on the final casting. Enclosed internal voids within a pattern, however, should not automatically be interpreted as a direct cause of porosity in the metal.
If a defect appears in exactly the same place on repeated castings, compare the original patterns, local geometry, and sprue arrangement before changing machine settings.
A Practical Troubleshooting Process
Step 1: Document the Defect
Photograph the casting before and after initial finishing. Record where the defect appears and whether it is localized or distributed throughout the piece.
Step 2: Classify What You Are Seeing
Determine whether you are looking at actual pores, an incomplete-fill defect, rough surface, inclusion, or another casting problem. Then note the shape, location, and distribution of any cavities.
Step 3: Record the Casting Process
For each test casting, record:
- Alloy
- Metal charge condition
- Metal temperature or relevant machine setting
- Flask temperature
- Investment brand and type
- Powder-to-water ratio
- Burnout schedule
- Pattern material
- Flask size
- Sprue arrangement
- Casting method
- Vacuum behavior, when applicable
Step 4: Change One Meaningful Variable at a Time
If you change the sprue design, temperatures, burnout schedule, investment preparation, and metal charge simultaneously, a different result will not tell you which change was responsible.
Controlled testing makes the process easier to understand and repeat.
Step 5: Keep a Casting Log
A simple casting log can reveal patterns between specific alloys, designs, sprue arrangements, burnout conditions, temperatures, and casting results. It is particularly useful when switching between different alloys or between wax and castable resin patterns.
Pre-Casting Troubleshooting Checklist
- Inspect the pattern surface for visible defects or contamination.
- Confirm that the sprue arrangement is appropriate for the pattern geometry.
- Pay particular attention to feeding heavier sections.
- Prepare investment according to the manufacturer's specified procedure.
- Allow the required investment setting time.
- Use a burnout schedule appropriate for the investment and pattern material.
- Consider flask size and furnace loading when following the burnout schedule.
- Confirm that furnace use and ventilation follow manufacturer requirements.
- Use an appropriate flask temperature for the specific casting process.
- Use clean metal prepared according to the alloy supplier's recommendations.
- Inspect the crucible and melting setup.
- Check the vacuum system for obvious leaks when vacuum-assisted casting is used.
- Record the process conditions before making the next test casting.
Frequently Asked Questions
Why do small holes appear after polishing a jewelry casting?
Filing and polishing can expose pores that were already below the original casting surface. The location, shape, and distribution of those pores can help determine which parts of the casting process should be investigated, but visual appearance alone may not identify the exact mechanism.
Can low vacuum cause porosity?
Poor vacuum performance can contribute to mold evacuation and incomplete filling in vacuum-assisted casting, but it is not a universal explanation for porosity. Shrinkage-related defects, metal-related gas porosity, investment reactions, and other process problems can occur independently of vacuum performance.
Does sprue size affect porosity?
It can. A feed sprue must help fill the mold and provide liquid metal while the casting solidifies. A feed path that freezes too early can contribute to shrinkage-related defects. The appropriate sprue design depends on the casting geometry, alloy, and process.
Can incomplete burnout contribute to porosity?
It can contribute to casting defects. Residual pattern material and interactions between residues, molten metal, and some investment systems may contribute to gas-related defects. Burnout should follow the recommendations for the specific investment and pattern material.
Is porosity always caused by the casting machine?
No. Porosity can originate from several stages of the process, including sprue design, metal preparation, investment, burnout, temperature, mold conditions, metal flow, and solidification. The casting machine is only one part of the complete system.
Final Takeaway
Successful porosity troubleshooting is less about finding one universal setting and more about identifying which part of the casting process is most likely contributing to the defect.
Pattern → Sprue & Feeding → Investment → Burnout → Metal & Melting → Temperature → Mold Filling → Solidification
Start with the specifications provided by your alloy, investment, and equipment manufacturers. Document each casting and change one meaningful variable at a time.
A controlled, repeatable process makes casting defects much easier to investigate and helps prevent the same problem from recurring.
0 comments